How to Source Custom Insulated Food Containers?
The global market for custom insulated food containers, stainless steel bento boxes, and thermal soup jars is expanding rapidly. Driven by modern lifestyle trends—such as meal prepping, outdoor dining, and a shift away from single-use plastics—consumers are actively seeking premium, reusable food storage solutions.
For private-label brands, corporate distributors, and Amazon top-sellers, sourcing high-quality thermal food containers offers higher average order values (AOV) and stronger profit margins compared to standard drinkware.
However, sourcing high-performance thermal containers requires understanding material properties, engineering standards, and precise manufacturing requirements.
This guide breaks down the step-by-step process of sourcing custom insulated food containers, the core advantages of stainless steel, key quality metrics to evaluate, and how to choose the right OEM/ODM manufacturing partner.
1. Define Your Product Architecture & Target Market
Before contacting manufacturers, clearly define your target audience and core product specifications:
- Capacity & Dimensions: Popular commercial sizes range from 400ml (14 oz) for personal snacks and soups to 800ml–1000ml (27–34 oz) for full family meals or bento sets.
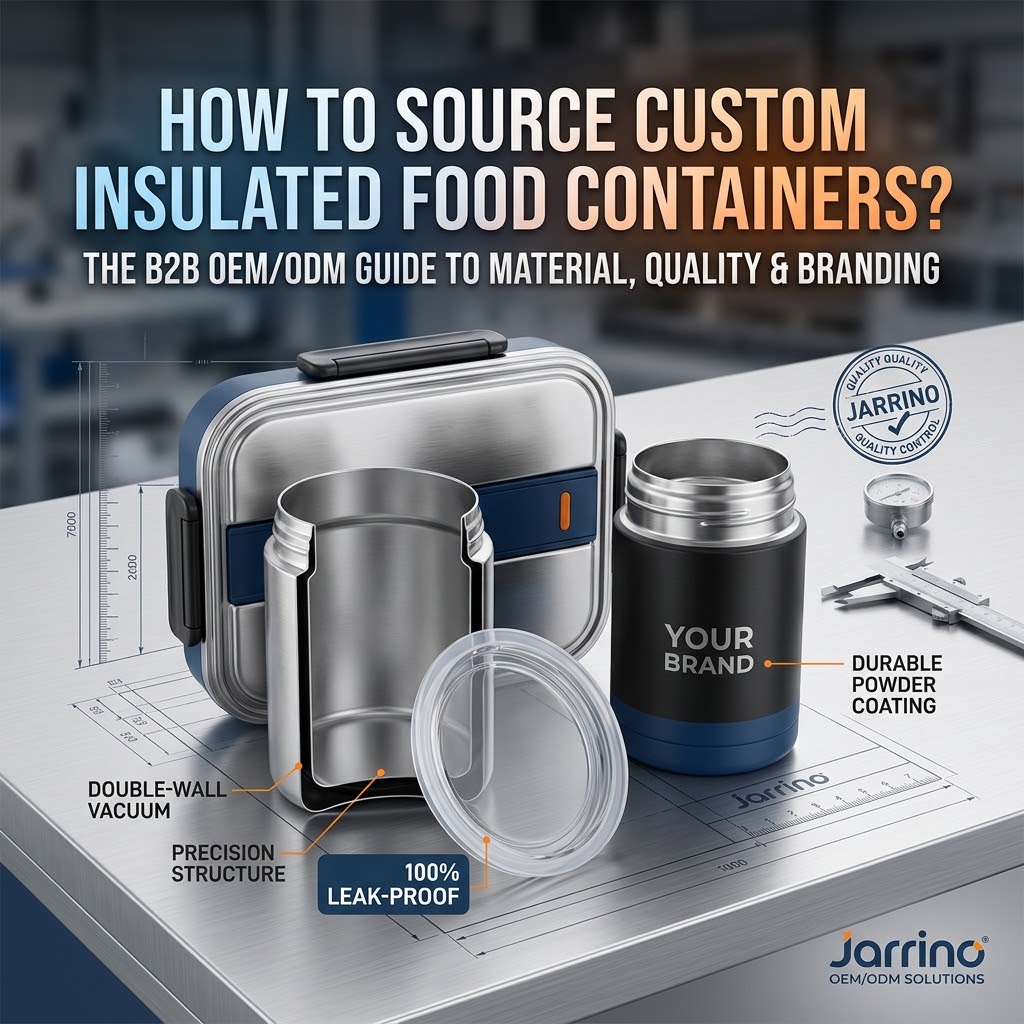
- Thermal Performance Standards: High-quality food containers utilize double-wall stainless steel vacuum insulation. Your containers should keep food hot for 6–12 hours or cold for up to 24 hours.
- Functional Feature Add-ons: Modern buyers expect wide-mouth openings (for easy eating and cleaning), pressure-release silicone vent buttons, and integrated foldable spoons or sauce compartments.
2. Key Advantages of Stainless Steel Food Containers
Selecting the right grade of stainless steel is essential for durability, safety, and brand reputation. Premium containers rely on food-grade 18/8 (SUS304) or medical-grade 316 stainless steel:
| Stainless Steel Advantage | Impact on Product Quality | Why It Matters for Your Brand |
| Non-Tox & Pure Taste | 100% BPA-Free & Chemical Resistance | Will not leach chemicals, toxins, or metallic flavors into hot foods and liquids. |
| Superior Corrosion Resistance | Resistant to Acids, Oils, and Salt | Prevents rust, pitting, and material breakdown when storing tomato soups, dressings, or salty dishes. |
| Exceptional Thermal Retention | Double-Wall Vacuum Barrier | Eliminates external condensation (sweating) while locking in temperature for extended hours. |
| Unmatched Durability | Dent and Impact-Resistant | Built for heavy daily use, outdoor camping, and longevity, reducing customer returns. |
3. Key Manufacturing Standards: How to Inspect Factory Quality
When reviewing sample kits or auditing supplier capabilities, focus on three critical engineering factors:
- Vacuum Leak & Pressure Decay Testing: Ensure the supplier conducts 100% automated pressure-decay tests during assembly to eliminate thermal insulation failures.
- Gasket Quality & Silicone Durometer: The seal must use 100% food-grade silicone (typically 40°–50° Shore A hardness) to prevent liquid oil degradation, aroma retention, and leaks during shipping.
- Coating Adhesion & Dishwasher Durability: Powder-coated or matte finishes must pass cross-hatch tape adhesion tests to ensure they won’t peel or scratch after repeated washing cycles.
4. Customization & Branding Options for Private Labels
To build a distinctive product line that commands premium retail pricing, select customized finishes tailored to your brand identity:
- Durable Outer Coatings: Choose between anti-slip powder coating, tactile 3D rubberized spray, or ceramic outer finishes.
- Branding & Logo Techniques:
- Laser Engraving: Permanent, crisp, and scratch-proof—exposing the raw stainless steel underneath.
- Silk-Screen & UV 3D Printing: Ideal for vibrant multi-color brand logos, patterns, or full-wrap artwork.
- Custom Packaging: Upgrade to eco-friendly color gift boxes, custom silicone carry handles, or insulated neoprene travel sleeves.
5. Partnering with the Right OEM/ODM Manufacturer
Sourcing custom insulated food containers successfully comes down to choosing an experienced manufacturing partner who supports your brand from CAD design to final shipment.
At Jarrino, we specialize in OEM/ODM production of high-performance stainless steel drinkware and thermal food storage. We offer:
- Turnkey Product Development: From 3D prototyping and custom mold engineering to mass production.
- Strict Quality Assurance: 100% inverted leak testing and thermal inspection on every production batch.
- Flexible MOQs & Fast Lead Times: Supporting both limited seasonal product launches and large-scale global retail rollouts.
Ready to Start Your Custom Food Container Project?
Expanding your brand into custom insulated food containers is one of the most profitable moves you can make this year. Work with a trusted supplier committed to technical precision and material quality.
[Contact the Jarrino OEM/ODM Team Today] to request sample kits, technical spec sheets, or custom manufacturing quotes.